Corrosion Coating for a Chlorine Plant in Johannesburg
Finding a corrosion coating chemical plant fumes won’t break down is the hard part of steel maintenance at a chlorine plant. So in April 2025, this Johannesburg site trialled Si-COAT 579 CM on its worst steel, while the plant kept running.
| Location | Johannesburg, Gauteng, South Africa |
|---|---|
| Industry | Chlorine processing |
| Exposure | Chlorine compounds, high humidity and constant surface contamination |
| Product | Si-COAT 579 CM, Traffic White |
| Applied | April 2025, one coat, no primer |
| Rollout | Process tank exteriors, after the trial |
| Checked | At three months, ten months and one year |
Download the full case study (PDF)
The problem: no coating lasted
The steel structure at this chlorine plant had a corrosion problem that normal coatings never solved. Chlorine fumes, high humidity and constant contamination broke down every coating before it gave real service life.
Three things made it harder. First, no earlier coating had lasted long enough to justify the cost and disruption of applying it. Second, chlorine makes hot work risky, so open flame, grinding sparks and abrasive blasting were out. Third, downtime was costly, so the plant had to keep running during the work.
In short, the client needed a coating that goes on cold, with no primer and no hot work. It also had to stand up to constant chemical exposure under live plant conditions.
The trial: corrosion coating in a live chemical plant
Rather than commit to a full job straight away, the client asked for a trial. TSS suggested the worst section of the plant, where chemical exposure is highest. That way, the corrosion coating faced the toughest chemical plant conditions on site before any wider rollout.
The crew used hand and power tools to remove loose corrosion and contamination. They did not blast or prime the steel. Instead, they applied one coat of Si-COAT 579 CM in Traffic White straight onto the cleaned steel, using standard brushes and rollers.
As a result, the job needed no hot work, no special equipment and no shutdown. Meanwhile, the plant stayed fully operational from start to finish.
Three months on: no breakdown
After three months, the coating in the worst section showed no sign of breakdown. There was no blistering, peeling, discolouration or loss of adhesion on the coated columns.
This mattered, because earlier coatings at this plant had already failed by the three month mark.
Ten months and a year on: chemical plant corrosion coating holds
At ten months, the coating looked the same as on the day it went on. Moreover, there was no corrosion creep, no coating failure and no maintenance in that time.
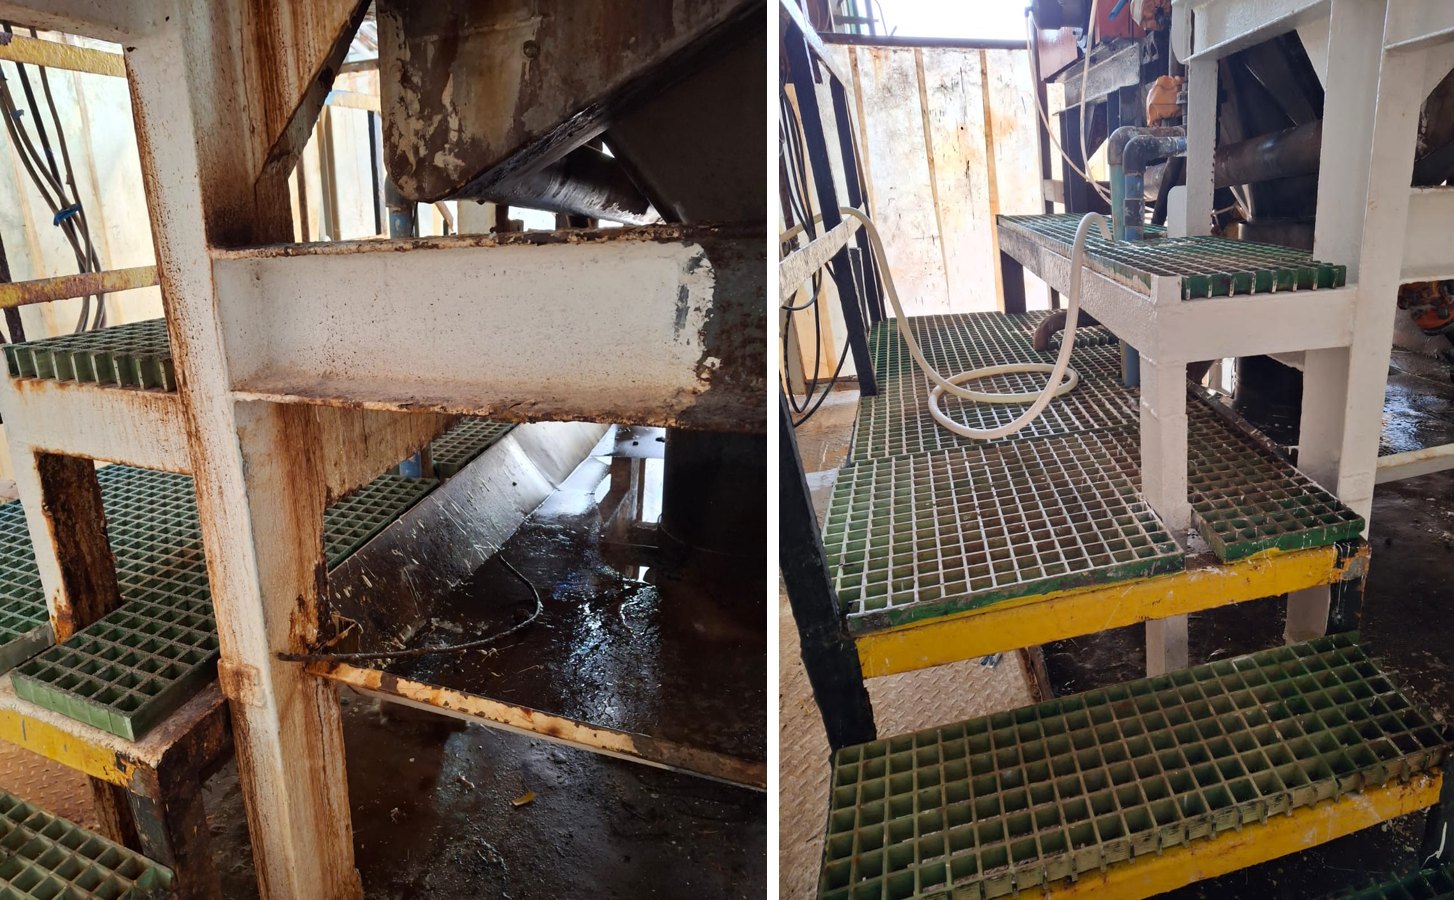
A year after application, TSS went back to check again. The steel was still clean, as the photo above shows.
The client also confirmed the following from the trial:
- Downtime stayed at a minimum during application.
- The crew needed no hot work at any stage.
- There was no primer before the coat.
- Equally, no topcoat went on after it.
- Finally, there was no hardener to mix, because 579 CM is a single component product.
After the trial: the plant coated its tanks
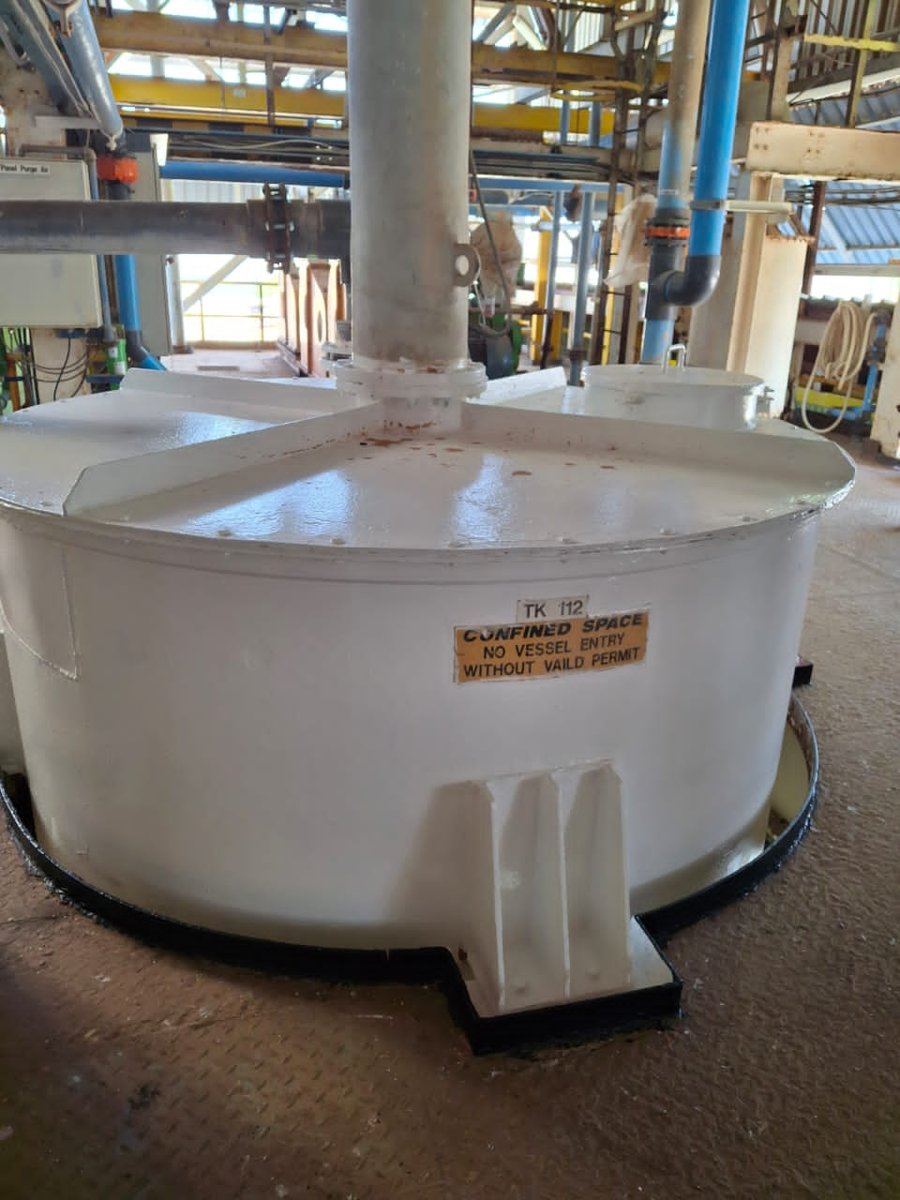
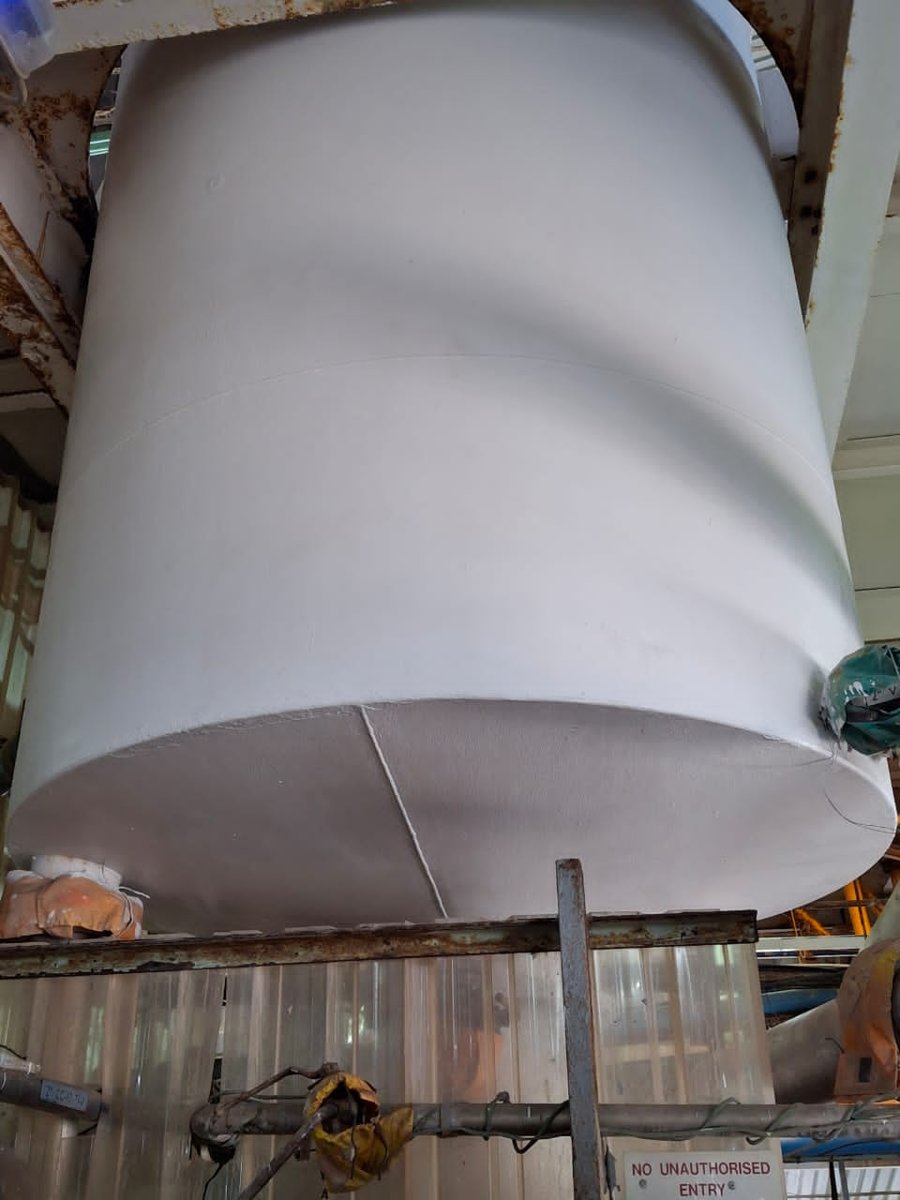
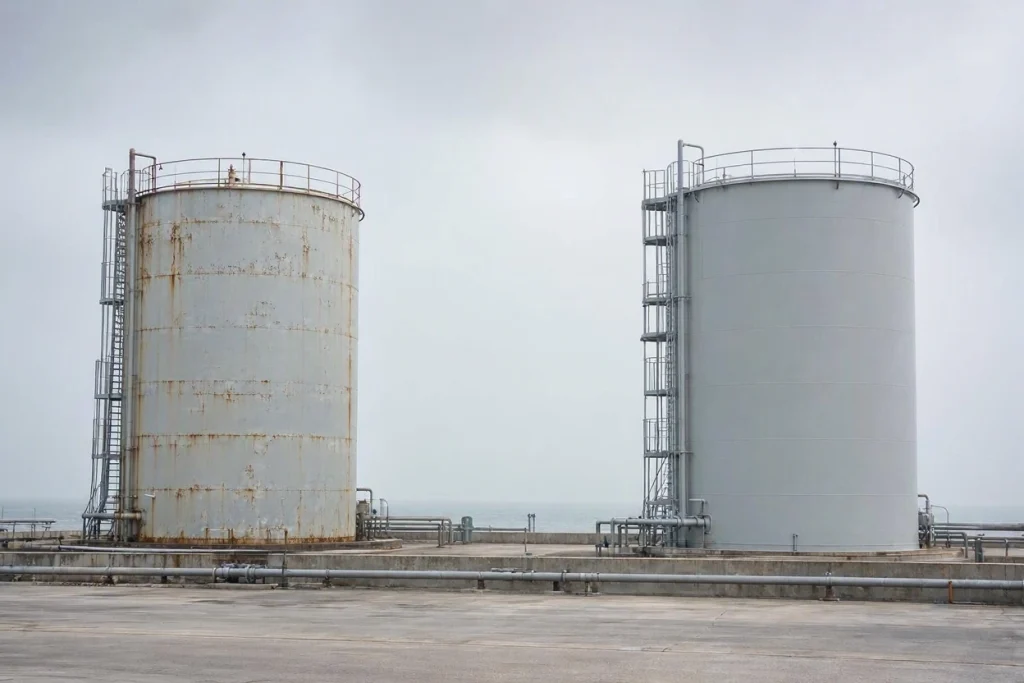
Once the trial results were in, the plant moved on to its process tanks. It coated the tank exteriors with the same Si-COAT 579 CM, again in Traffic White. Below are two of them: a floor standing tank and the underside of an elevated tank.
Why this corrosion coating works in a chemical plant
Si-COAT 579 CM is a single component, moisture cure RTV silicone coating made by CSL Silicones. CSL designed it for corrosion maintenance, and its silicone binder behaves very differently from epoxy, polyurethane and alkyd systems under chemical attack.
Organic binders break down under chlorine fumes, chlorides and acid vapour. As a result, epoxy films tend to blister and lift, while polyurethanes lose their mechanical strength. Silicone, by contrast, keeps its adhesion and elasticity in the same conditions.
The coating also stays flexible after it cures. Plant steel expands and contracts with temperature changes and vibration from running equipment. Rigid coatings crack under that movement, which lets chemicals get in underneath. In contrast, 579 CM moves with the steel, so it doesn’t crack.
Because it only needs hand or power tool cleaning, 579 CM suits sites where blasting is risky or not allowed. Similarly, the same product works as both primer and finish, so one product does the whole job. For full details, see our silicone corrosion coating page and the Si-COAT 579 CM FAQ.
Key takeaways
Chemical resistance doesn’t come standard with most coatings. In a chemical plant, a corrosion coating gets it from the binder chemistry, and that is where silicone beats epoxy and polyurethane.
Moreover, with no hot work and no primer, the coating can go on in hazardous areas without shutting the plant down.
Finally, a year of clean steel in the worst part of a live chlorine plant is a result earlier coatings never reached at this site. Field results like this tell you more than lab data alone.
For more proof, read how the same coating held up at the Hoopstad fertiliser plant and on a hopper in Durban harbour. Also see the Florida power plant piping, still unchanged after 20 years, and the Florida Fence Test results.
Frequently asked questions
Can a corrosion coating go on in a live chemical plant?
Yes. Si-COAT 579 CM goes on cold as a single component coating, with no hot work, no abrasive blasting and no special equipment. So you can apply it to prepared steel while the plant keeps running. That suits sites where downtime is costly and hot work is a safety risk.
Does Si-COAT 579 CM need a primer?
No. It bonds straight to steel cleaned with hand or power tools. You still have to remove loose rust and contamination, but you don’t need to blast or prime. At this chlorine plant, nobody used a primer, and there was no adhesion loss after a year. For C5 High exposure, however, CSL specifies the full CM System with CSL 979 primer.
How does silicone compare with epoxy in a chemical plant?
Epoxy cures rigid, and chlorides, acids and alkalis attack it over time. It also cracks under heat movement and vibration, which lets chemicals in under the film. Silicone, however, resists these chemicals far better and stays flexible. At this plant, 579 CM stayed intact for a year in chlorine service, where earlier coatings had failed.
What surface preparation does 579 CM need?
The minimum is hand or power tool cleaning (SSPC SP2 or SP3) to remove loose rust, loose mill scale and contamination. The surface must also be clean and dry before you start. Because there is no blasting or primer, a normal maintenance crew can do the prep without special equipment. Our guide to steel surface preparation explains more.
Which chemical plant sites suit this corrosion coating?
Si-COAT 579 CM handles chlorides, chemical fumes, and acid vapour and occasional splash. So it suits structural steel in petrochemical plants, fertiliser plants, water treatment works, mineral processing plants and other aggressive sites. Keep in mind it is for above ground steel only, not immersion.
Where can I get Si-COAT 579 CM?
Technical Solution Supplies distributes CSL Silicones products across Southern Africa, including the DRC and the Seychelles. For pricing, technical data and application support, request a quote.
More corrosion protection articles
- Corrosion Coating Cost: How to Compare Quotes on Total Cost of Ownership

- Corrosion Protection in South Africa: Comparing the Methods That Actually Work

- Corrosion Protection Coating South Africa: Everything You Need to Know
- Corrosion Resistant Coating for Mining: Protecting Copper Operations Across Southern Africa
- Mining Corrosion Protection in South Africa: Why SI-COAT 579 CM Outperforms Traditional Coatings

- Anti-Corrosion Coating for Structural Steel: Why Silicone Outperforms Epoxy


Send us the problem
Photos and a rough size are enough to start, while drawings and specs can follow later. Then we come back with the right product and a quote.